Confirm the selected heating medium and supply boundary
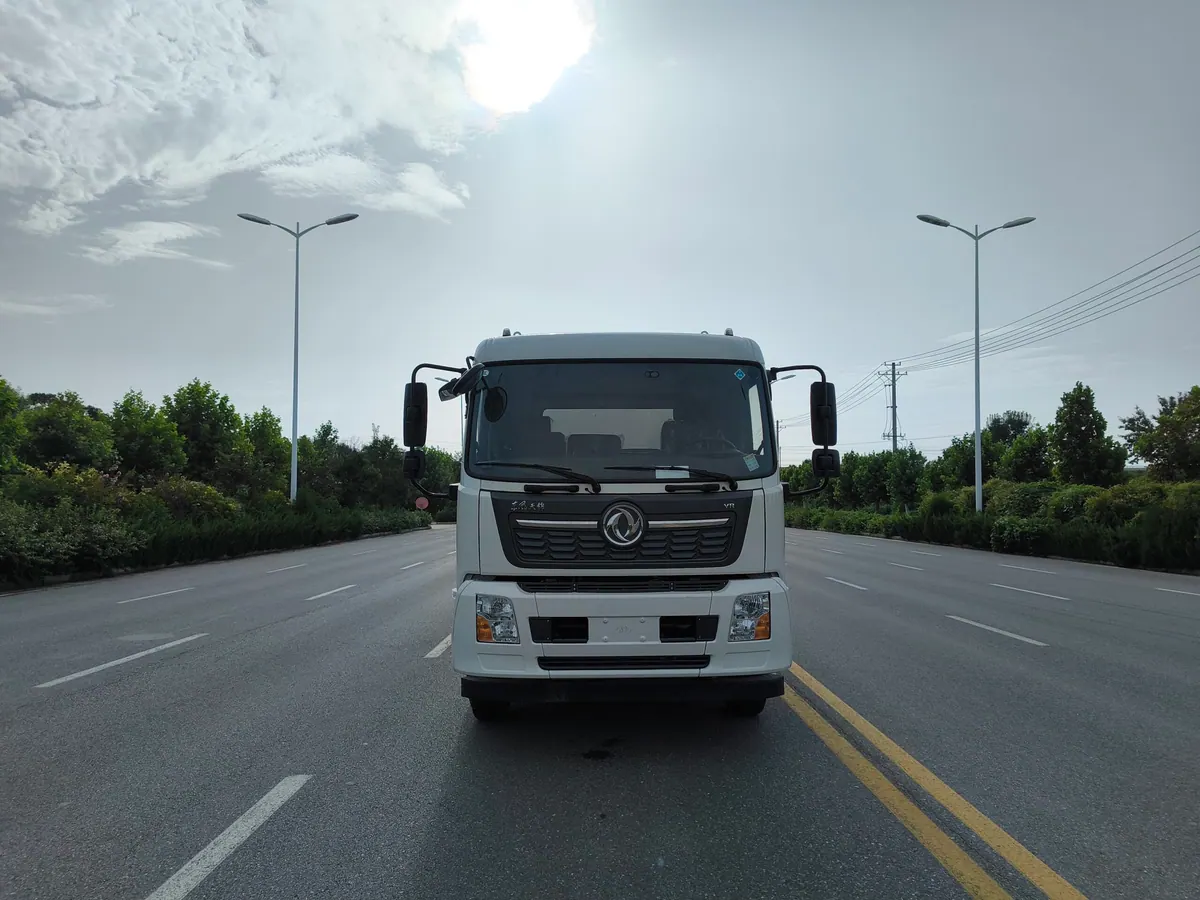
The oilfield boiler truck is a configured mobile heat source. Establish the required steam, hot-water or separately approved thermal-fluid arrangement and the actual useful duty before choosing equipment. The media are not assumed interchangeable or simultaneously available. A steam-focused review applies only to an identified steam configuration; a general boiler label does not establish a complete hot-oil circulation or wax-removal package.
Confirm the actual boiler, burner, fluid system and control functions in the offer. Water treatment, dual-fuel capability, winter equipment and destination documentation are not assumed standard. Assign distribution, receiver, return-handling and site installation responsibilities explicitly, with relevant evidence and competent project review for the complete arrangement.
Start with the job decision
Oilfield Boiler Truck projects succeed when the equipment scope is tied to a defined operating duty: supplying the selected mobile heating duty with an accepted medium, receiving arrangement and operating basis. A useful project document separates normal duty, maximum credible duty, standby or transient conditions and the physical interfaces available at site. This keeps procurement language connected to field reality.
Record required steam output, working pressure and steam quality, available feedwater quality and fuel availability as ranges rather than isolated peak figures. The supplier can then explain how the duty-selected boiler or heating assembly, burner selected for the specified fuel, specified feedwater and conditioning interfaces and identified onboard control functions work together across the intended envelope.
Agree the FAT plan before manufacturing is complete
The inspection and test plan should identify hold points, witness points, acceptance criteria, required instruments and records. A FAT is not simply a visual factory visit. It should verify that the manufactured package matches approved documents and that controls and protection functions behave as agreed.
| Review item | What to confirm | Evidence or input |
|---|---|---|
| duty-selected boiler or heating assembly | Selected medium, useful output and acceptance boundary | Configuration-specific duty response |
| burner selected for the specified fuel | Actual fuel and supported combustion arrangement | Provider selection and supply information |
| specified feedwater and conditioning interfaces | Accepted analysis, supply and conditioning responsibilities | Actual water and fluid boundary schedule |
| identified onboard control functions | Actual indication, alarm and action scope | Function schedule and verification evidence |
Functional tests should follow the operating sequence
Test permissives, startup logic, normal control, alarms, controlled shutdown and emergency shutdown in a sequence that operators can recognize. Simulate relevant low, high and signal-failure conditions. If full-load testing is not practical at the factory, document the limitation and define the site acceptance test that will close it.
Do not release shipment with undocumented gaps
Compile signed test sheets, material and calibration records, final drawings, manuals, spare-parts lists, packing lists and the punch list. Classify open items by whether they prevent shipment, prevent installation or may be closed during commissioning. Photographs help, but they do not replace signed acceptance records.
Keep a usable project record
Maintain one controlled file containing the approved duty sheet, supplier clarifications, drawings, component data, inspection records, test results, deviations, photographs and signed acceptance documents. Record document revisions and the person responsible for each open item. This prevents the operating team from receiving a package whose final configuration differs from the information used during procurement.
The handover set should also identify installed component models, consumables, calibration intervals, recommended spares, preservation requirements and supplier support contacts. Capture baseline operating readings when the unit is accepted. Those records give maintenance personnel a reference for condition changes and allow later modifications to be reviewed against the original design basis.
Before closing the project, confirm that operators can find the startup, normal-operation, controlled-shutdown and emergency procedures relevant to their unit. Training attendance alone is not sufficient; the responsible team should demonstrate the required checks and know which conditions require escalation rather than continued operation.
Codes, standards and project requirements
Confirm the final specification and acceptance plan against the owner’s project standards, local jurisdiction and ASME Boiler and Pressure Vessel Code resources. The applicable project documents govern whenever they are more specific.
Carry the agreed factory findings into the installation and commissioning review, keeping external interfaces, authorized site work and remaining acceptance evidence clearly assigned.